Explore our high-performance industrial chemicals manufactured to strict international standards.
High-purity chemical synthesis intermediate designed for pharmaceutical and industrial applications.
Superior thermal stability and anti-oxidation performance for demanding industrial heating systems.
Manufactured under strict quality protocols for specialized chemical synthesis uses globally.
Premium fine chemical raw material widely used in polymer and organic electronic manufacturing.
Essential reducing agent applied in electroless plating and chemical reaction accelerators.
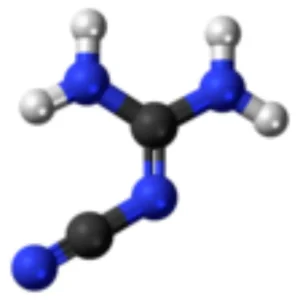
High-grade curing agent and pharmaceutical intermediate exported globally with consistent quality.
Efficient industrial solvent offering excellent solvency for resins, coatings, and extractions.
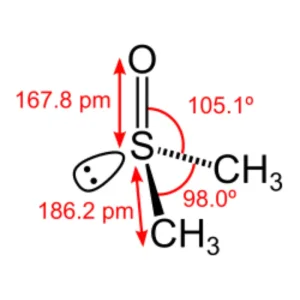
Versatile polar aprotic solvent with exceptional dissolving power for organic and inorganic compounds.
Founded in December 2004, Shandong Saier Chemical Technology Development Co., Ltd. has embarked on an impressive journey since its establishment. Situated at No.207, WeiLiu Road, Qilu Chemical Industrial Park, Linzi, Zibo City, Shandong Province, the company has continuously evolved and thrived in the highly competitive chemical and industrial gas supply chain ecosystem.
In early times, with a registered capital of 60 million yuan, the company laid a solid financial foundation. Initially focusing on the production of basic chemical products, the initial product lineup included environmentally friendly high-boiling aromatic solvents (Solvent naphtha, TOPSOL, KOCOSOL, Aromatic Hydrocarbon, TOLUENE AROMATIC HYDROCARBON, NAFTA DISOLVENTE SOLVESSO) such as S-100, S-150, S-150ND, S-180 and S-200, Heat transfer oils L-QC320, and other main intermediate products along with products like durene, PVC plasticizers, thiophene, 1,3-Cyclohexanedione, MIPK, TMOF, TMOA, HPA, and TMG.
These products were mainly sourced from major refineries and aromatic plants such as Sinopec, PetroChina, ChemChina, Zhejiang Petrochemical, and Hengli Petrochemical. By leveraging these reliable raw material sources, the company was able to ensure product quality from the start. At that time, the production capacity was 720,000 tons per year, and the products were sold in domestic markets including Beijing, Shanghai, Tianjin, Hebei, Shandong, Henan, and to major enterprises like Sinopec and PetroChina, while actively expanding to global markets across Asia, Europe, America, and Southeast Asia.
As the years passed, Shandong Saier Chemical Technology Development Co., Ltd. recognized the critical importance of innovation and technological advancement. It began to invest significantly in research and development, aiming to improve production efficiency, enhance product quality, and develop greener, more sustainable solutions.
In response to the growing global demand for energy-saving and environmentally friendly products, the company optimized its entire production workflow. By introducing cutting-edge rectification and separation technologies, we successfully reduced carbon emissions, minimized waste generation, and secured recognition as a national high-tech enterprise, validating our industry authority and technical prowess.
Our strategic placement within the Qilu Chemical Industrial Park grants us unmatched supply chain resilience. Direct pipeline connections with tier-one petrochemical giants guarantee continuous feedstock supply, shielding our operations from external market volatility and ensuring on-time delivery for international B2B buyers.
Looking toward the next decade, the industrial gas and chemical manufacturing sectors are undergoing a profound transformation driven by digital automation, carbon neutrality mandates, and advanced material sciences. Our strategic roadmap focuses on three core pillars:
Industrial gases and high-boiling aromatic solvents serve as the invisible backbone of modern manufacturing. Our product ecosystems are deployed across diverse localized scenarios worldwide:
Providing specialized solvency for automotive coatings, industrial paints, and high-performance resins across European and Asian manufacturing hubs.
Supplying low-naphthalene aromatic solvents engineered to optimize pesticide emulsion stability and environmental compliance.
Powering heavy industrial heat transfer systems with L-QC320 thermal oils ensuring prolonged operational safety.
Explore our extended portfolio tailored for specialized industrial manufacturing requirements.
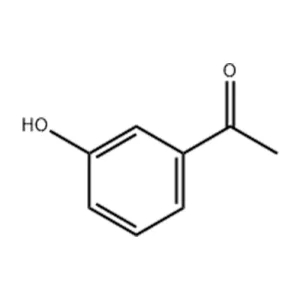
Reliable chemical intermediate supplied with complete technical documentation and batch analysis.
High solvency power and controlled evaporation rate for industrial formulation needs.
Precisely synthesized fine chemical intermediate meeting exacting purity standards.
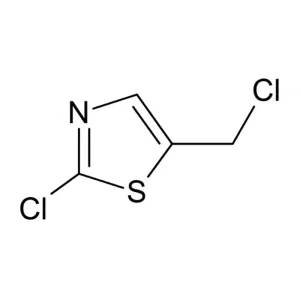
Vital organic building block utilized widely in advanced synthesis sectors.
Essential raw material for polyimide films, high-temp insulation, and advanced polymers.
Heavy aromatic fluid engineered for specialized industrial cleaning and formulation applications.
Heterocyclic compound widely applied in pharmaceutical and agrochemical manufacturing.
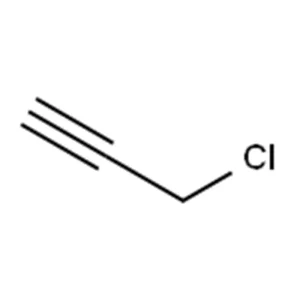
Reactive intermediate manufactured under rigorous safety and quality controls.
Get expert insights into our manufacturing standards, logistics capabilities, and quality assurance protocols.
We boast over two decades of manufacturing expertise, a massive 720,000-ton annual capacity, and strategic partnerships with top refineries like Sinopec and PetroChina, ensuring consistent quality, competitive pricing, and uninterrupted supply security.
Our production facilities operate under strict ISO and national high-tech environmental standards. Every batch is rigorously tested in our advanced laboratories, accompanied by comprehensive COA, MSDS, and REACH-compliant documentation for seamless global export.
We provide flexible global logistics solutions including ISO tank containers, drum shipments, and bulk vessel transport, supported by experienced export teams ensuring safe and timely delivery to Asian, European, American, and Southeast Asian markets.
Yes. Leveraging our advanced fractional rectification technology and R&D capabilities, we can tailor aromatic solvent cuts and chemical intermediates to meet your exact technical specifications.
Ready to optimize your industrial supply chain? Contact our engineering and sales team today for custom quotes, technical data sheets, and sample requests.
 Saier Chemical